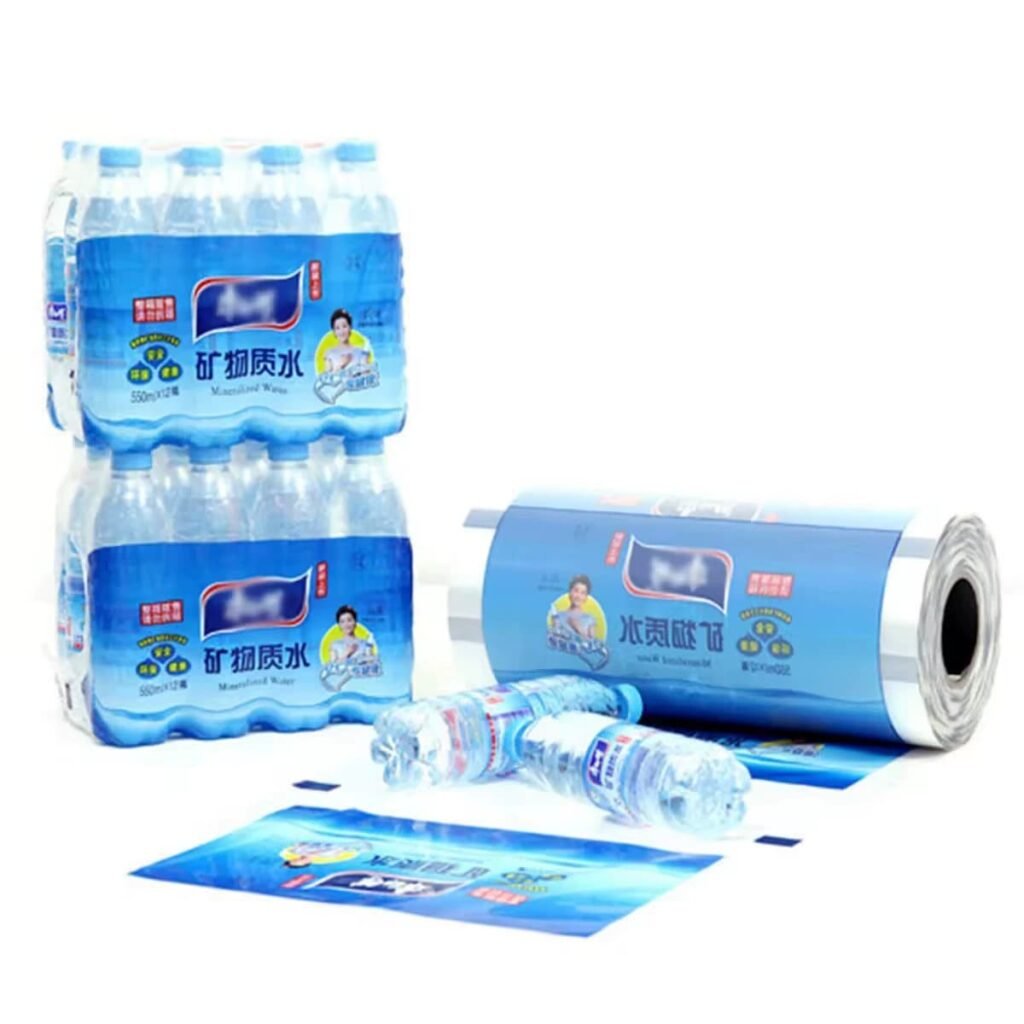
When you buy PE shrink film, one of the most critical technical parameters you need to understand is the shrink ratio — specifically, how much the film shrinks in the machine direction (MD) versus the transverse direction (TD). Getting this right directly determines whether your packages look tight and professional or wrinkled, loose, and uneven.
What Is MD and TD?
Machine Direction (MD) is the direction the film travels through the extruder and winder during production. This is the length of the roll.
Transverse Direction (TD) is the width direction of the film, perpendicular to the MD.
When heat is applied in a shrink tunnel, the film shrinks in both directions. The ratio of MD shrinkage to TD shrinkage is engineered during production and must match your packaging requirements.
Why Shrink Ratio Matters
If the MD-to-TD shrink ratio is wrong for your product shape and bundle configuration, you will experience:
- Excess MD shrinkage — the film pulls too tight along the length, causing necking, film breakage, or crushed product
- Excess TD shrinkage — the sides pull in too much, creating side fins and uneven bundling
- Unbalanced shrink — the package twists or tilts inside the tunnel
- Loose bundles — insufficient shrink in either direction means the film does not hug the product
Typical Shrink Ratios for PE Shrink Film
PE shrink film can be engineered for different shrink profiles depending on the application:
| Application | Typical MD Shrink | Typical TD Shrink | Notes |
|---|---|---|---|
| Bottled water multipacks | 8–15% | 15–25% | Higher TD for tight wrap around bottles |
| Canned beverage bundles | 10–18% | 20–30% | Stronger TD for cylindrical cans |
| Carton/tray packaging | 5–12% | 10–20% | Moderate for rectangular shapes |
| Heavy industrial goods | 3–8% | 5–12% | Lower shrink for protection, not tightness |
| Printed promotional packs | 8–15% | 15–22% | Balanced for print registration |
These ranges are starting points. The exact specification depends on your shrink tunnel temperature, conveyor speed, product geometry, and bundle weight.
How Shrink Ratio Is Engineered
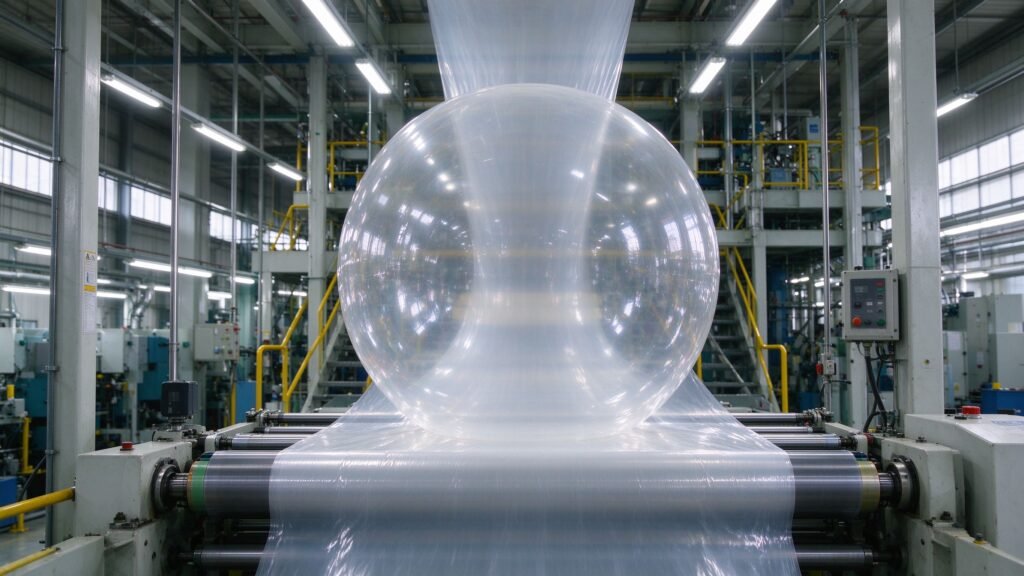
During the blown film extrusion process, the bubble height, air ring cooling rate, and frost line position all influence the molecular orientation — and therefore the shrink behavior — of the finished film.
By adjusting:
- Extrusion temperature profile
- Bubble blow-up ratio (BUR)
- Cooling air flow rate
- Winding tension
Manufacturers can tune the MD/TD shrink balance to match specific packaging line requirements.
Matching Shrink Ratio to Your Packaging Line
To select the right shrink ratio, you need to provide:
- Product shape — round bottles, square cartons, irregular items
- Bundle configuration — how many units per pack, arrangement
- Shrink tunnel settings — temperature (typically 150–180°C for PE), conveyor speed
- Desired appearance — tight retail look vs. protective industrial wrap
- Film width and layflat dimensions — overhang on the product
Common Shrink Ratio Problems
Wrinkles on the top and bottom of the bundle — usually indicates insufficient MD shrink or tunnel temperature too low.
Film breaks at the seal line — could mean excessive TD shrink pulling on the seal, or film thickness insufficient at the seal area.
Side fins or wings — TD shrink too high relative to MD, or film width too wide for the product.
Bundle twists in the tunnel — MD/TD balance is off, or the film roll has uneven tension causing it to pull sideways.
Requesting a Custom Shrink Ratio
If your application is unusual — irregular product shapes, high-speed lines, or specific appearance requirements — you can request a custom MD/TD shrink balance.
Tell us about:
- Your product and bundle dimensions
- Your shrink tunnel temperature and line speed
- What you are currently experiencing (wrinkles, breaks, loose bundles)
- Sample packs if available
We will recommend a film specification with the appropriate shrink ratio for your line.
Get the Right Shrink Specification
Shrink ratio is not a one-size-fits-all number. The correct PE shrink film specification depends on your product, your tunnel, and your packaging line speed.
[Contact our team](/contact/) with your packaging details, and we will recommend the right MD/TD shrink balance for your application. You can also [request a sample](/contact/) to test on your line before placing a bulk order.